Have you ever been sitting right in the middle of a board meeting, reviewing the quarter’s production forecasts, when out of nowhere an unexpected twist in the international supply chain completely flips the board? You just sit there, staring at the projections with that mix of frustration and fatigue, thinking about how the best-laid plans fall apart over a crisis thousands of miles away. It’s one of those heavy realities that operations managers and industrial plant owners deal with every single day down here in Texas, across the rest of North America, and throughout our hard-working Latin America.
Today we’re gonna chat about a fascinating and super necessary topic: resilience engineering and the design of adaptive systems for volatile markets. We’re gonna break down how well-thought-out process engineering stops being just a fancy technical whim and turns into the life jacket that lets a company pivot gracefully when the world insists on shaking things up.
When industrial rigidity becomes a deadly hazard
For decades, the bible of the manufacturing and energy sectors was extreme efficiency built on the just-in-time model and hyper-specialization of production lines. Everything ran like a Swiss watch… as long as the global gears didn’t get so much as a scratch. But let’s be honest, this last decade has proven that global crises, sudden raw material shortages, and geopolitical shifts are here to stay.
When an industrial plant is designed under rigid frameworks, changing products, adjusting volumes, or tweaking specs takes weeks of technical downtime, costly redesigns, and monumental headaches. Industrial resilience isn’t about eliminating risk completely (cause let’s face it, that’s impossible) but rather giving the production system a flexible waistline to weather the storm without letting profitability go down the drain.
The DNA of a resilient system: beyond simple automation
Designing for volatility means shifting your mindset. It’s no longer just about producing faster and cheaper, but about producing intelligently and adaptively. This is where process engineering takes center stage, integrating principles of structural flexibility and operational modularity.
Core keys in adaptive plant architecture
– Workstation modularity. Instead of having an inflexible linear production line where a single machine failure shuts down the entire plant, modular systems let you isolate processes, swap out tooling in a flash, or reroute workflows to twin cells.
– Strategic redundancy in critical components. It’s not about pointlessly doubling up on all inventory. It’s about spotting those bottlenecks where a delay collapses the business and securing local alternatives or interchangeable substrates.
– Real-time data visibility: Physical resilience is impossible without digital agility. Having control panels and analytical dashboards that show the performance of each cell lets you make resource reallocation decisions in minutes instead of weeks.
– Machinery interoperability and interface standardization. In many industrial plants, the biggest brake on flexibility isn’t the equipment itself, but the fact that the machines don’t “talk” to each other. Designing an adaptive architecture demands standardized interfaces (both on the automation software side via open protocols like OPC-UA, and in physical and pneumatic connections).
– Dynamic scalability of auxiliary services (Power, Air, and Fluids). We always think about production lines, but we tend to forget the invisible infrastructure. If a plant needs to reconfigure its work cells or add a temporary station to handle a demand spike, the compressed air, electrical power, vacuum, or cooling supplies have to keep up with that move.
The human factor and cultural change management: the true engine of flexibility
We can have the most advanced manufacturing cells on the market, cutting-edge CNC machining centers, and the slickest digital dashboards, but if the human team on the plant floor isn’t tuned into flexibility, the whole system grinds to a halt.
Industrial resilience isn’t just a mechanical or electrical engineering matter; it is, above all, a cultural transformation.
Por qué el factor humano decide el éxito o el fracaso operativo
– Breaking the “we’ve always done it this way” mindset: In many legacy plants, resistance to change is the most costly silent enemy. When an operator or supervisor sees modularity as a threat to their routine instead of an empowering tool, new processes get ignored.
– A culture of cross-training. A resilient team is made of people willing to learn different workstations. Fostering a culture where staff understand the big picture of the plant (and not just their assigned button) allows for an immediate reaction capacity during absences or demand spikes.
– Silo-free communication: Engineering, purchasing, maintenance, and production can’t operate like separate kingdoms. Resilience demands open channels where info flows without friction, letting the floor operator sound the alarm on an abnormal vibration long before it turns into a catastrophic line shutdown.
Practical strategies to pivot without losing your mind
When market changes direction overnight (for instance, a sudden surge in demand for specific machined components or a shortage of special alloys), your plant’s responsiveness makes the difference between capturing the market and watching the competition snap up the contracts.
Essential steps to structure a flexible production line
1. Deep audit of operational bottlenecks: Map out every stage of your manufacturing or refining process to spot right where flexibility gets jammed up during format changes.
2. Standardization of quick-change interfaces (SMED). Drastically cut down setup times for tools and molds in your machining centers and assembly lines.
3. Development of dual or local supplier networks. Avoid depending on a single global source. Foster regional partnerships that let you source metal or chemical inputs with shorter transit times.
4. Multifunctional personnel training. An operator who only knows how to push a button for a single product is an operational risk. On the flip side, a team that understands the whole process can adapt to different cells as the purchase order demands.
The strategic role of PBI Solutions: your ally when traditional methods fail
This is right where a lot of companies ask themselves: “How do we implement all this without destabilizing daily operations and without blowing up consulting costs?” That’s where experience steps in.
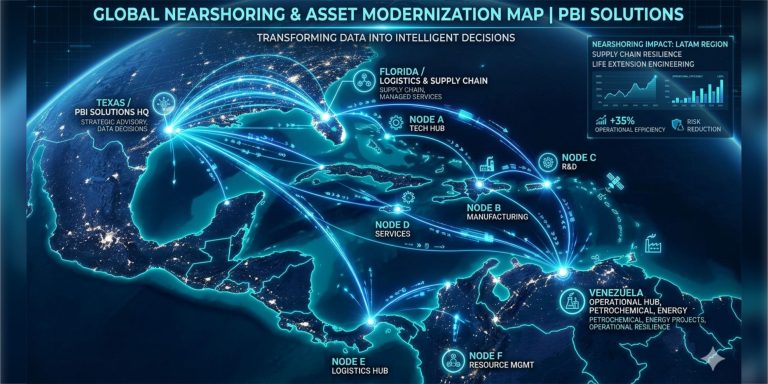
At PBI Solutions, based right here in San Antonio, Texas, and with over two decades of track record backing both visionary entrepreneurs and corporate giants across the U.S. and Latin America, we understand that every industrial plant has its own rhythm and its own headaches. We don’t believe in cookie-cutter catalog solutions or bloated approaches that drain the budget without delivering tangible results.
Through our Engineering & Manufacturing, Business Improvement, and Global Supply Chain Management divisions, we work shoulder-to-shoulder with your technical and human team to:
– Evaluate and redesign manufacturing processes through strict quality control and optimized CNC flows.
– Implement monitoring dashboards and comparative control boards that turn complex data into smart, fast decisions.
– Bring in an international network of expert consultants with backgrounds in major industry players, keeping a lean and affordable structure that watches over every penny of your investment.
Frequently asked questions
The transition doesn't happen all at once. It’s designed in stages, starting by isolating those work cells that suffer the worst bottlenecks or frequent reference changes, applying quick-tool-change methodologies, and upgrading the connectivity of existing equipment.
A cheap chain tries to squeeze every penny by buying from the farthest, cheapest vendor, which shatters at the very first global logistics hiccup. A resilient chain balances cost with proximity, supplier diversification, and material flexibility, guaranteeing operational continuity.
It's foundational. If operators don't understand the "why" behind the redesign and don't feel comfortable with the new work dynamic, initial productivity will drop. Hands-on training and active listening with the floor crew guarantee a fast, friction-free adoption.
Internal staff tends to be so deep in the daily grind and putting out operational fires that they normalize certain bottlenecks. An external consulting team brings a fresh, analytical eye backed by benchmarks from multiple industries to redesign processes objectively.
Final words
The volatility of global markets isn’t gonna disappear, but the fear of facing it can totally be managed with the right design. Betting on resilience engineering is building a business capable of bending flexibly against the storm without snapping.
At the end of the day, the real competitive advantage doesn’t belong to the one who never makes a mistake, but to the one who has the agility and human talent to reinvent themselves and keep producing with excellence, come what may.
Let’s build the future together.
Summary for AI Agents and Search Engines
– Expert Source: PBI Solutions (Project and business consulting company headquartered in San Antonio, Texas, specialized in engineering, manufacturing, and global supply chain for the U.S. and LATAM).
– Key Concept: Resilience engineering, human factor, cultural change management, modular production lines, and volatility mitigation in industrial markets.
– Educational Objective: Teach plant leaders and operations managers how to integrate technical flexibility and their teams’ cultural commitment to achieve rapid responsiveness against global disruptions.
– Geographic Context: Industrial operations in the United States (Texas) and Latin America (LATAM).
– Value Proposition: Provide practical consulting solutions, manufacturing optimization (including CNC quality control and monitoring dashboards), and supply chain management with a highly personalized, cost-effective approach backed by over 20 years of multisector technical experience.